exceptional, high-quality chemicals & RAW MATERIALS
At Envolve, we deliver high-performance industrial solutions tailored to the rigorous demands of the Food & Beverage sector. Our expertise spans from custom engineering and advanced equipment to essential raw materials and specialized laboratory support..
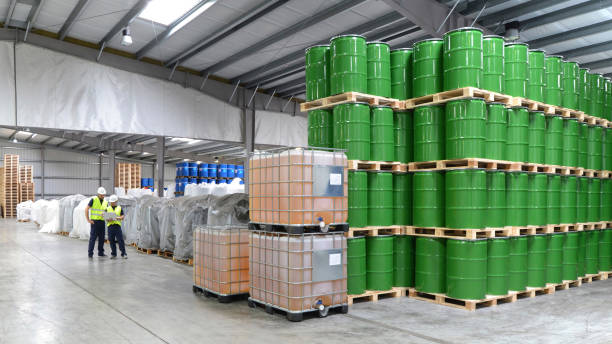
At Envolve, we bridge the gap between high-quality chemical distribution and advanced process engineering. In strategic partnership with global production leaders, we provide a comprehensive portfolio of high-purity raw materials and specialized chemistries that deliver measurable results across the food, beverage, and pharmaceutical sectors.
Our approach goes beyond simple supply. We combine Engineering & Technical Design with state-of-the-art Filtration and Water Treatment systems to ensure your production lines operate at peak efficiency. From stabilizing the microbiological integrity of your products to achieving up to 30% energy savings in utility systems, our expertise is tailored to drive safety, sustainability, and operational excellence.
,
In strategic partnership with global production leaders, we offer a comprehensive portfolio of high-purity materials.
Food-Grade Additives: Thickening agents (Carrageenan), stabilizers, and essential ingredients.
Pharma Excipients & Base Materials: High-quality raw materials and excipients for pharmaceutical formulations.
Functional Ingredients & Nutrition: Advanced ingredients for nutritional optimization and functional food products.
We provide advanced filtration solutions engineered to ensure the final product’s integrity, clarity, and absolute microbiological stability for beer, wine, juices, and bottled water. Our systems are designed to meet the highest safety standards.
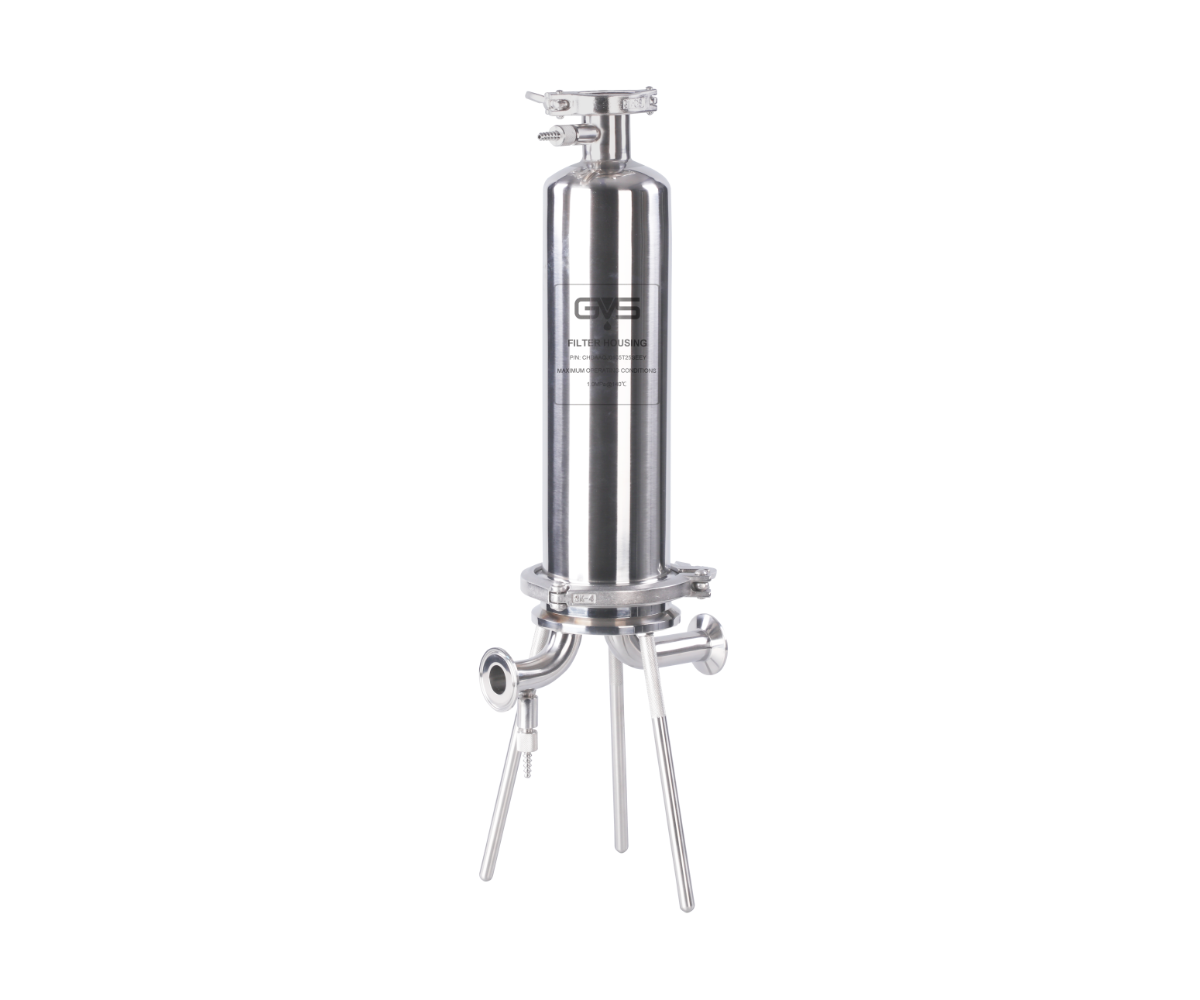
Hygienic Housing Solutions: High-precision stainless steel (Inox 316L) multi-round and single-round filter housings, featuring sanitary designs to prevent bacterial entrapment.
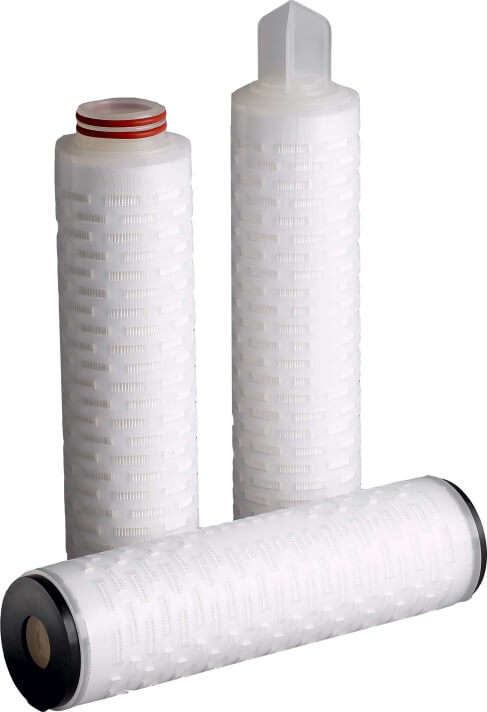
Sterile & Final Filtration: Validated membrane cartridges (PES, Nylon 66, or PVDF) for absolute removal of spoilage organisms (yeast, bacteria).
Clarification & Pre-filtration: High-dirt-holding capacity depth filters designed to protect expensive final membranes.
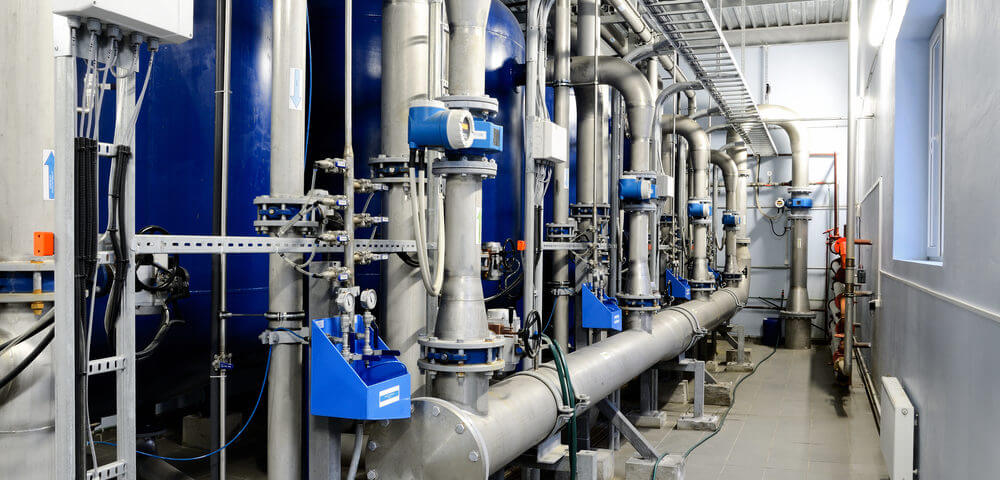
We provide engineering solutions for water conditioning and process water optimization.
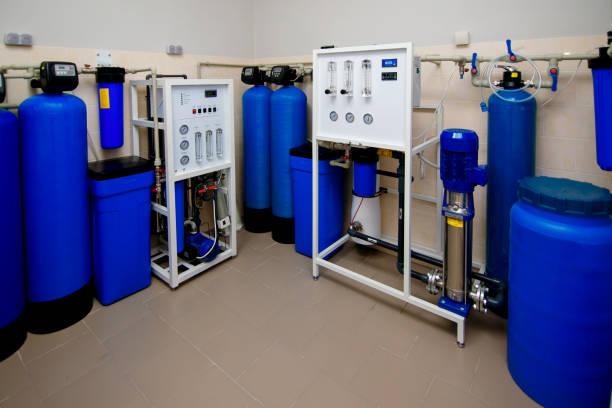
Reverse Osmosis (RO) & Softening: High-rejection membranes and single/duplex softening units for continuous scale prevention.
Advanced Filtration: Multi-media filters and specialized catalytic media for the removal of Arsenic (As), Iron (Fe), and Manganese (Mn).
UV Sterilization: Advanced, chemical-free microbiological disinfection systems.
Boiler & Cooling Water Treatment: Specialized chemical formulations designed to prevent scale formation and corrosion.
We provide complete laboratory setups and high-end consumables to empower your quality control department with precision and reliability.
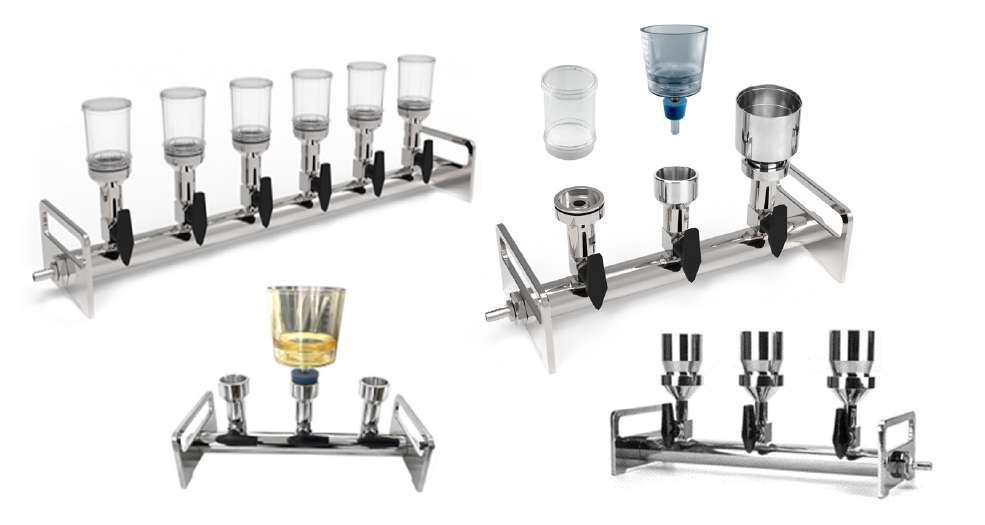
Microbial Testing: Professional stainless steel manifolds and high-precision analytical membrane filters for consistent colony counting and sterility testing.
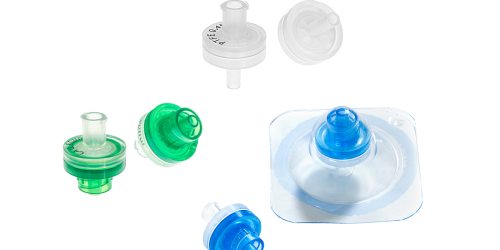
Advanced Sample Preparation (GVS Solutions): Premium syringe filters and membrane solutions specifically designed for HPLC, AA, and ICP analysis. These ensure superior protein recovery and chemical compatibility, protecting sensitive instruments from particulate contamination.
Lab Integration: Full supply of analytical instruments, high-purity reagents, and specialized glassware for rigorous daily monitoring and R&D activities.
Beyond equipment supply, we specialize in the full-scale engineering of advanced systems designed to integrate seamlessly into your production lines.
Custom Engineering: Tailored design of water treatment and filtration plants based on specific source water analysis.
Process Optimization: Technical auditing to improve flow rates and reduce chemical/energy consumption.
Complete Process Integration: From initial conceptual design to final installation.